
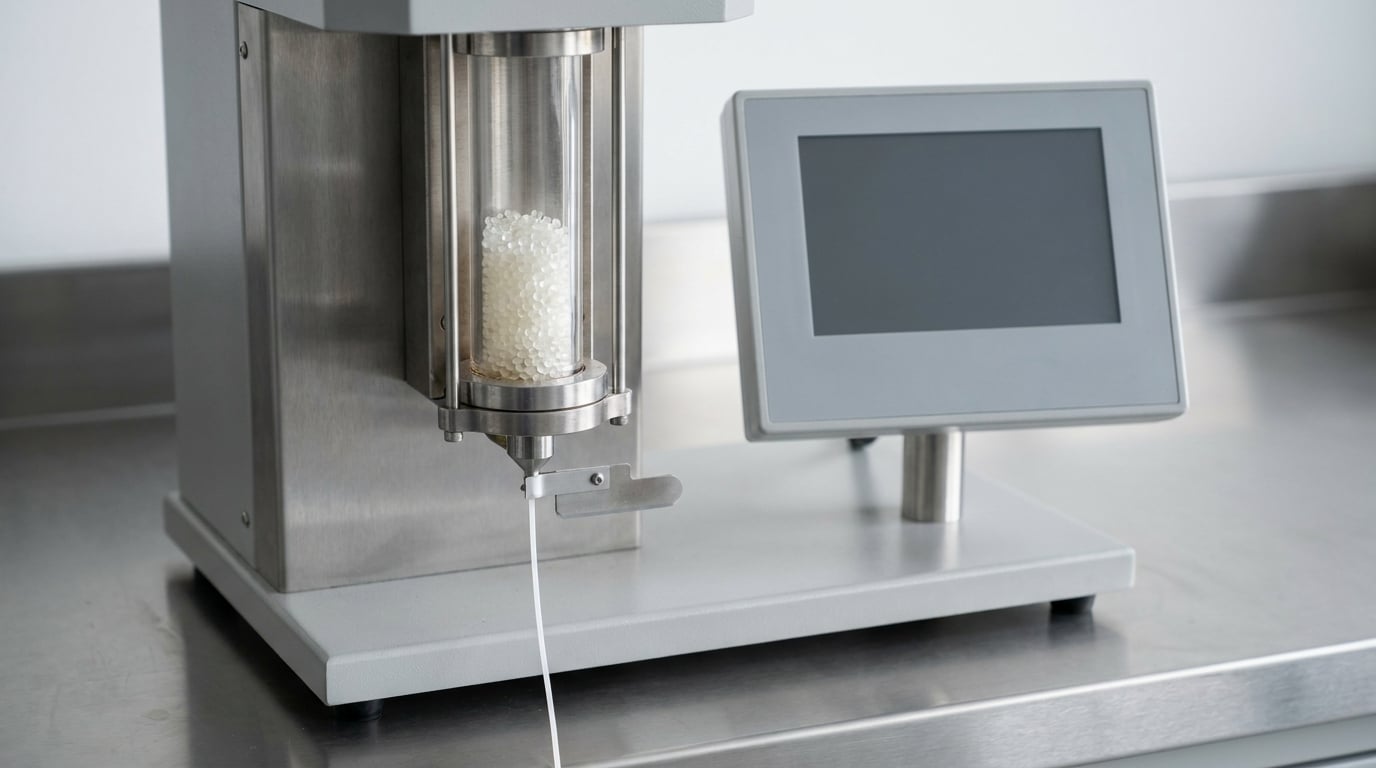
Most people land on a resin datasheet looking for what melt flow index tells you about a resin, and find one number on the page. That number is the mass of molten polymer, in grams, that a standard capillary die extrudes in ten minutes under a set temperature and load. A higher MFI means lower melt viscosity and, generally, a lower average molecular weight, so the resin fills thin walls and thin sections easily. A lower MFI means more resistance to flow and more melt strength in the extrudate. That is the whole number in one sentence, and everything else on the datasheet around it decides whether the number means anything to your process.
The catch most people miss: an MFI value on its own is close to meaningless. The temperature, the test load and the method sit behind it, and two MFI numbers measured under different conditions are not the same measurement. Before anything else, read the condition, not the value.
Table of Contents
- What Is Melt Flow Index?
- How Melt Flow Index Is Measured
- What Does Melt Flow Index Tell You About a Resin?
- How to Interpret High, Medium, and Low MFI Values
- Does a Higher Melt Flow Index Mean a Better Resin?
- What Melt Flow Index Does Not Tell You
- How to Use MFI in Resin Selection and Quality Control
- Frequently Asked Questions
- Is a higher melt flow index better for plastic processing?
- Why can two resins with the same MFI behave differently?
- What ASTM or ISO standard is used to test melt flow index?
- Does melt flow index indicate molecular weight directly?
- How much MFI variation is acceptable for an incoming resin batch?
- Can melt flow index replace viscosity or rheology testing?
- Conclusion
What Is Melt Flow Index?
The melt flow index, also called melt flow rate (MFR), is the mass of molten polymer in grams that a standard capillary die extrudes in ten minutes under a specified temperature and load. It is a single-number screen of how fluid the melt is at that one point in the process window, not a full description of the material.
Three conditions travel with the number, and all three change the result:
- Temperature — commonly 190 °C or 210 °C for polyolefins, 230 °C or 235 °C for PET, 275 °C for some ABS grades, and higher still for engineering resins.
- Load — the weight driving the piston, usually 2.16 kg or 21.6 kg. The heavier load pushes harder and produces a much higher flow figure for the same material.
- Die geometry — a standard capillary of 2.160 mm diameter, used unless the supplier reports a modified die.
So a datasheet line reading “MFI 7 g/10 min (190 °C/2.16 kg)” carries a completely different meaning from “MFI 7 g/10 min (230 °C/21.6 kg)”. Different physics, different material state, different number.
Melt flow index is a mass rate, not a viscosity. It is inversely related to melt viscosity, which makes it a convenient stand-in: a resin with a high MFI at the test conditions behaves, in a rough way, like a lower-viscosity melt under the same conditions.
How Melt Flow Index Is Measured
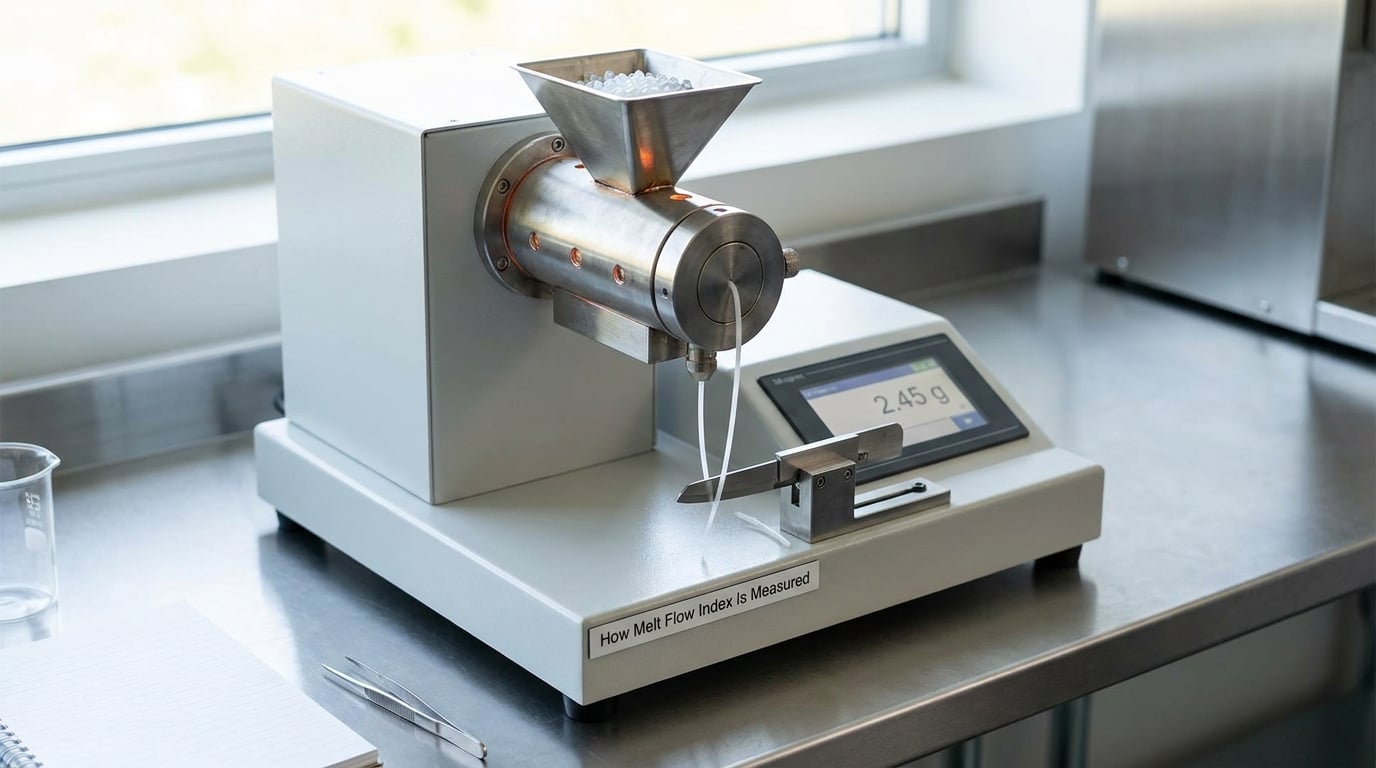
The test is standardised as ASTM D1238 in the United States and ISO 1133 internationally, and the two are close enough in method that most datasheets cite one or both. The sequence is the same in every lab I have looked at:
- Dry and clean the sample. Moisture is the most common source of a bad number, especially with polyamides, PET and polycarbonate. A wet sample hydrolyses in the barrel and reads high.
- Load the pellets into the barrel and pack them with the standard plunger so no air voids sit against the die.
- Heat to the test temperature and hold until the melt is fully homogeneous. Time matters here, because not every grade finishes purging in the same number of minutes.
- Purge until a continuous, free-flowing strand comes out of the die.
- Apply the test load (2.16 kg or 21.6 kg) and let the flow stabilise.
- Cut and weigh the extrudate over a timed interval, usually in the cut-off string method, and report the result in g/10 min.
Why the load distinction matters so much: the 2.16 kg and 21.6 kg loads do not just scale the answer, they sample the material differently. A stiff, high-molecular-weight grade may read barely a few tenths of a gram per ten minutes under 2.16 kg and several grams under 21.6 kg. If your supplier quotes 190 °C/2.16 kg and a competitor quotes 190 °C/21.6 kg, you are comparing two different properties.
Because of this, I only trust a MFI comparison when the temperature, the load and the standard all match. Anything else is a guess dressed up as data.
What Does Melt Flow Index Tell You About a Resin?
Short answer: it tells you how the melt will move at the test conditions. Everything downstream follows from that — viscosity, the tendency to fill a cavity, the resistance to sag, the expected surface finish, and roughly how the molecular weight sits.
Four practical things fall out of the number:
Apparent melt viscosity. Higher MFI, lower viscosity at the test point. That is the direct relationship, and it is why an unfilled low-MFI grade can leave a short shot in a thin-wall mould where a higher-MFI grade fills cleanly.
Average molecular weight, indirectly. Longer chains tangle more, resist shear, and flow less. That is why high-MFI grades generally sit at the lower end of the molecular weight range for their family, and why MFI is sometimes used as a rough proxy when a direct molecular weight measurement is not available.
Process response. The number tells you whether the melt will likely be easy to pump and fill, or stiff and demanding. It does not describe the whole shear curve, and it says nothing about how the material behaves far from the test condition.
Batch-to-batch consistency. When repeated test results sit within a narrow spread, the melt is consistent, and a stable process is easier to hold. This is often more valuable to a buyer than the absolute figure, and it matches what the practical filament and compounding community keeps coming back to: buyers care most about repeatability.
| What you see | Higher MFI | Lower MFI |
|---|---|---|
| Melt viscosity at test conditions | Lower | Higher |
| Average molecular weight (general trend) | Lower | Higher |
| Cavity filling in thin sections | Easy, low short-shot risk | Demanding, short shots likely if the process is cold |
| Melt strength and draw-down resistance | Low — more sag, more drool, harder to hold a parison | High — holds shape under gravity and pressure |
| Extruder pressure and screw torque | Lower | Higher, and closer to the machine limit |
| Surface finish and melt fracture tendency | Good flow, but very fluid melts can streak | Excellent draw-down, higher risk of melt fracture at high output |
| Typical mechanical expectation | Lower stiffness and tensile strength | Higher stiffness and strength |
Read that table as a direction, not a specification. Every row is a tendency at a fixed test condition.
How to Interpret High, Medium, and Low MFI Values
The only way “high” or “low” means anything is inside a polymer family. An MFI of 12 is an extremely stiff polyethylene and a perfectly fluid polypropylene. The ranges below are typical commercial territory at standard test conditions, and they are a starting point for comparison, not a specification.
| Polymer family | Typical MFI range (g/10 min) | Where grades in that range tend to land |
|---|---|---|
| HDPE | 0.3 to 40 | Blow moulding and film at the low end; injection moulding, caps and thin-wall packaging toward the high end |
| LDPE | 0.5 to 100 | Film, coating and extrusion at the low end; injection moulding and rotomoulding higher up |
| LLDPE | 0.5 to 30 | Blown film, stretch film, pipe and rotational moulding |
| PP homopolymer | 1 to 100 | Raffia and fibre spinning low; injection moulding, caps and appliances higher |
| PP copolymer | 1 to 40 | Injection moulding and twin-screw applications needing toughness |
| PS | 2 to 30 | Packaging, houseware and foam applications |
| ABS | 2 to 30 | Injection moulded housings, automotive interiors, pipe fittings |
| PC | 6 to 20 | Optical, electrical and structural parts where clarity and stiffness matter |
| PET | 0.2 to 1.0 (hydrolytic, measured differently) | Preform bottle grades, commonly reported as intrinsic viscosity rather than MFI |
| PA6 and PA66 | 5 to 200 | Low values for film and carpet; high values for thin-wall and fibre spinning |
| POM | 10 to 200 | Gearing, conveyor parts and precision mouldings at the high end |
PET is worth a note: it is hygroscopic and thermally sensitive, so the industry usually reports intrinsic viscosity rather than MFI, because molecular weight is what actually governs the preform and bottle performance. If someone offers you a PET grade with an MFI but no intrinsic viscosity, ask for the viscosity number.
Now pair the number with the process. The ranges below sit inside each family, not across all of them:
| Process | Usual MFI territory (g/10 min) | Why |
|---|---|---|
| Injection moulding | 8 to 50 | Fast fill and low part weight; high flow reduces cycle time |
| Extrusion (pipe, profile) | 0.5 to 10 | Melt strength keeps the extrudate dimensionally stable after the die |
| Blown film | 0.3 to 6 | Draw-down needs a melt strong enough to resist necking and bubble instability |
| Blow moulding | 0.3 to 2 | Parison extrusion and hang strength dominate over filling speed |
| Fibre spinning | 10 to 40 and above | High flow through spinneret capillaries at high line speeds |
| Filament extrusion (3D printing) | Workable but narrow | Too stiff and the drive slips; too fluid and diameter control drifts |
The trade-off is always the same pair of words: flow versus melt strength. Take the highest MFI you can live with, not the highest MFI available. A grade one step too fluid will make your life harder through sag, drool, weld-line weakness and dimensional drift, and that cost shows up faster than a short shot ever does.
For 3D-printing filament specifically, a small mismatch shows up as consistent minor over-extrusion rather than a dramatic failure, which is exactly the kind of drift that gets misdiagnosed for weeks. One r/Creality user described tuned flow rate as the other key after a successful build, with untuned flow producing “consistent minor over extrusion” on grid infill crosses. That is a flow-characteristics problem, and MFI is the first number to look at.
Does a Higher Melt Flow Index Mean a Better Resin?
No. MFI is not a quality score, a strength rating, or a measure of how good the resin is. A higher MFI usually means a lower average molecular weight, and lower molecular weight typically means lower tensile strength, lower stiffness and less toughness.
Higher MFI wins when the job is filling. Thin-wall packaging, small injection mouldings, high-speed cycles and fine-detail parts all benefit from a fluid melt, and a stiff grade simply will not fill the geometry at an acceptable cycle time.
Lower MFI wins when the melt has to hold its shape. Blown film, bottle preforms, parison extrusion and fibre spinning all need draw-down strength. A very high-MFI grade there produces sagging, unstable bubbles, poor wall thickness distribution and, in film, a roll that varies across the width.
So the better resin is the one whose flow behaviour matches your tooling, your temperature range and your filling requirement. A meaningful MFI specification comes from a process question, not a shopping decision.
What Melt Flow Index Does Not Tell You
This is the section most datasheets skip, and it is where specifications go wrong. MFI is one point on a rheological curve. It cannot give you the rest of the curve, and it cannot stand in for a mechanical or thermal data sheet.
What a single MFI value does not tell you:
- Molecular weight distribution. Two resins with an identical MFI can have very different chain-length distributions, and therefore very different shear thinning, die swell and melt fracture behaviour. A narrow distribution and a broad distribution can print the same number.
- Mechanical properties. Tensile strength, flexural modulus, impact resistance and elongation are not derivable from MFI. Datasheets exist precisely because these are measured separately.
- Stabilisation and degradation state. Antioxidant level, thermal stability and prior thermal history are invisible to the melt flow test.
- Contamination, colour and inclusion quality. Black specks, gels, unmelted particles and colour consistency do not register.
- Long-term durability. Hydrolysis resistance, weathering and creep tell you nothing from a ten-minute test.
- Filler, pigment and masterbatch effects unless the datasheet value was measured on the compounded product rather than the base resin.
MFI also has close cousins that answer questions it cannot:
| Metric | What it reports | When to ask for it instead |
|---|---|---|
| MFI / MFR | Mass extruded in 10 minutes, g/10 min | Default datasheet value, and the one every supplier can quote |
| MVR | Volume extruded in 10 minutes, cm³/10 min | Density varies with lot; MVR is denser-independent and sometimes preferred in Europe |
| Intrinsic viscosity / GVR | Flow resistance of a dilute solution, tied to molecular weight | PET and fibre polymers, where molecular weight governs end performance |
| Capillary rheometer sweep | Full viscosity against shear rate at several temperatures | Any serious process development, or when one MFI point is not enough |
If your application is demanding, one MFI number plus a full capillary sweep tells you far more than the MFI alone. It also maps your processing window: if the viscosity curve is steep across the temperature range, the material is forgiving; if it barely moves, you have little room to correct a cold barrel with heat.
How to Use MFI in Resin Selection and Quality Control
Here is the workflow I would follow, in order, whether you are buying a grade or releasing incoming batches.
1. Get the datasheet and read the whole line. Not just the number. You want the standard (ASTM D1238 or ISO 1133), the temperature, the load, and whether the figure is on the base resin or the compounded grade. A datasheet with a bare MFI and no conditions is a reason to ask questions before you sample anything.
2. Fix your process requirement first. Write down the process, the thinnest wall you must fill, the maximum melt temperature you can run, and whether the melt has to hold shape after the die. From that you get a target range, not a single number — something like 8 to 20 g/10 min at 230 °C/2.16 kg for a thin-wall moulded part.
3. Compare like with like. Only compare values measured at the same temperature, load and method. If a supplier will not state the conditions, treat the number as unusable for comparison regardless of how attractive it looks.
4. Establish an internal acceptance range. Most production specs set a band, commonly something like ±5% or ±10% around the nominal value, plus an absolute ceiling. Tighten it for critical applications and for recycled feedstock. The spread matters more than the midpoint, because a drifting melt is what changes your process settings week to week.
5. Test incoming batches and trend the data. A single result tells you little. A running chart over time tells you whether the supplier is stable, whether a lot change is real, and whether your own storage and drying are contributing. Investigate drift before the parts start drifting.
6. Validate in your own process. MFI narrows the candidates. It does not approve one. Run the short-shot trial, the fill-pattern check, the draw-down trial, whatever your part actually needs, before you commit to a production volume.
For troubleshooting, the bridge from number to symptom is worth keeping in your head:
| Symptom on the machine | Likely flow-related cause |
|---|---|
| Short shots in thin sections | MFI too low for the wall thickness, or barrel temperature too low |
| Sagging, drool, poor parison control | MFI too high — the melt cannot hold its own weight |
| Melt fracture, sharkskin on extrudate | Excessive shear rate against a high-viscosity melt, or a die surface issue |
| Excessive die swell and poor dimensional control | Broad molecular weight distribution at a given MFI |
| Screw slippage, inconsistent drive | Melt viscosity too high for the available torque |
| Rising MFI batch over batch | Thermal degradation, or a rising recycled content in the feed |
| Colour streaking, specks | Poor dispersion from a carrier or filler mismatch — not an MFI problem at all |
That last row is the one people misdiagnose most often. A masterbatch whose carrier resin is a poor match for the base polymer changes dispersion and appearance, which gets blamed on flow. Matching the carrier MFI to the base resin, within a sensible tolerance, resolves more of these cases than any additive change.
On recycled material, a rising MFI is usually the interesting signal rather than a good one. Chain scission from repeated heat history lowers molecular weight, so the number climbs while strength falls. If your recycled feed is drifting upward, you are watching degradation accumulate, and a chain extender or a tighter sorting step is the fix, not a higher-flow virgin to blend in.
Frequently Asked Questions
Is a higher melt flow index better for plastic processing?
No. A higher melt flow index means lower melt viscosity and a lower average molecular weight, which helps thin sections fill but reduces melt strength, stiffness and tensile performance. Higher MFI suits thin-wall injection moulding, fine detail and fast cycles. Lower MFI suits blown film, parison extrusion, pipe and fibre spinning, where the melt must hold its shape after leaving the die. The right value depends on your geometry, tooling and temperature range, not on a general ranking of grades.
Why can two resins with the same MFI behave differently?
Because MFI is a single point on a viscosity curve, not a full description of the melt. Two grades with the same reported MFI can have different molecular weight distributions, which changes shear thinning, die swell and melt fracture behaviour. Additives, fillers, stabilisers and pigment loading also shift real processing behaviour without appearing in the base resin number. Compare the full datasheet and, where the application is sensitive, run a capillary rheometer sweep across shear rates and temperatures.
What ASTM or ISO standard is used to test melt flow index?
ASTM D1238 is the US standard and ISO 1133 is the international one. The methods are closely aligned, and many datasheets cite both. The standard governs sample conditioning, barrel temperature, piston load, capillary die dimensions and the timed cut-off and weighing step. Always check which one the supplier used, along with the temperature and the load, since those conditions change the reported number far more than the choice of standard does.
Does melt flow index indicate molecular weight directly?
Not directly. MFI is an indirect proxy that works because longer polymer chains tangle more and resist shear, so they flow less. That relationship is a trend within a polymer family, not a calculation. Two resins of different families with the same MFI can sit at entirely different molecular weights. Where molecular weight itself is the deciding property, ask for a direct measurement such as intrinsic viscosity, or a gel permeation chromatography result, rather than inferring it from melt flow.
How much MFI variation is acceptable for an incoming resin batch?
Most production specifications set a band around the nominal value, commonly plus or minus five or ten percent, and many add an absolute ceiling. Tighten the band for critical parts and for recycled feedstock, where thermal history makes the melt less predictable. Judge the supplier on the trend across many batches rather than on any single result, because a stable supplier with a wider band is often safer than one that swings around a tight nominal.
Can melt flow index replace viscosity or rheology testing?
No, and treating it as a substitute is a common source of failed trials. MFI measures mass flow at one temperature, one load and one approximate shear rate. A capillary rheometer sweep gives you viscosity across a range of shear rates and temperatures, which is what you need to map a processing window, predict pressure drop and set screw speed. Use MFI for screening and batch control, and use rheology for process development and troubleshooting.
Conclusion
Melt flow index is a useful screening and batch-control signal, not a complete resin specification. It tells you how the melt moves at one temperature under one load, and the conditions behind the number decide whether you can compare it to anything else. Start by reading the test condition, then the full datasheet, then confirm the grade in your own process. If one number has to survive on its own, choose a consistent melt with a tight batch spread over a slightly better-looking value from an untested supplier.