
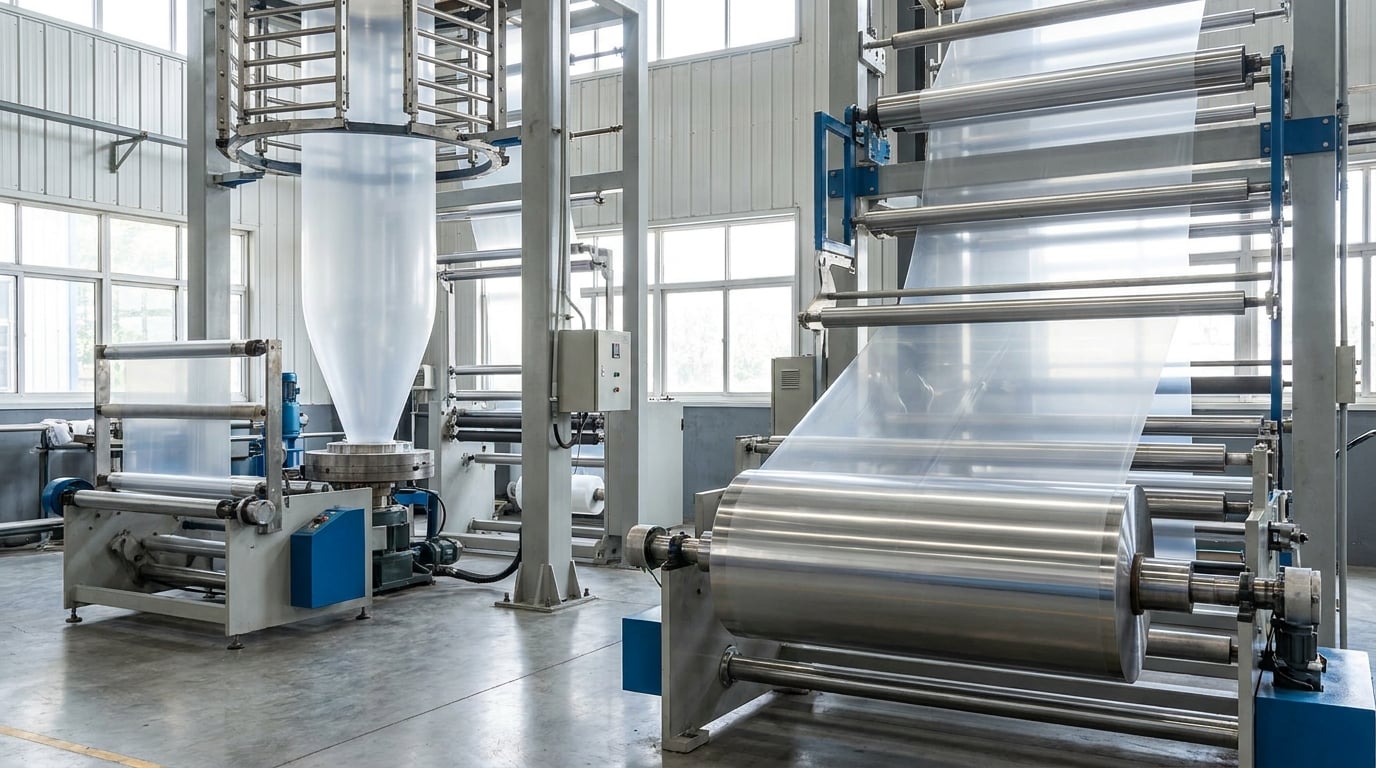
The main blown film vs cast film differences come down to how the melt is formed. Blown film is inflated into a bubble through a circular die and pulled in two directions at once, which gives it tear strength and load memory. Cast film is laid as a flat sheet onto chilled rolls, which gives it clarity, quiet unwind and very thin gauges.
Both routes usually run the same resin, most often linear low-density polyethylene (LLDPE). So this is not a resin comparison, it is a process comparison, and picking the wrong one shows up as tears on a wrapped pallet or as a haze complaint on a display pack rather than in a lab sheet.
The audience here tends to be operations and engineering: the people choosing film for a wrapping line, specifying a bag, or deciding whether a new extrusion line should be blown or cast. Everything below is written for that decision.
Table of Contents
- Blown Film vs Cast Film Differences at a Glance
- How Blown Film and Cast Film Are Manufactured
- Thickness Control, Film Quality, and Consistency
- Strength, Stretchability, and Barrier Performance
- Optical Properties, Sealability, and Processing Behavior
- Production Speed, Changeovers, and Cost Comparison
- Which Should You Choose?
- Frequently Asked Questions
- Is blown film stronger than cast film?
- Which process produces better optical clarity?
- What film thickness is typically made with blown or cast extrusion?
- Can blown film and cast film use the same plastic resin?
- Which process is better for printing and heat sealing?
- How do manufacturers test the differences in film performance?
Blown Film vs Cast Film Differences at a Glance
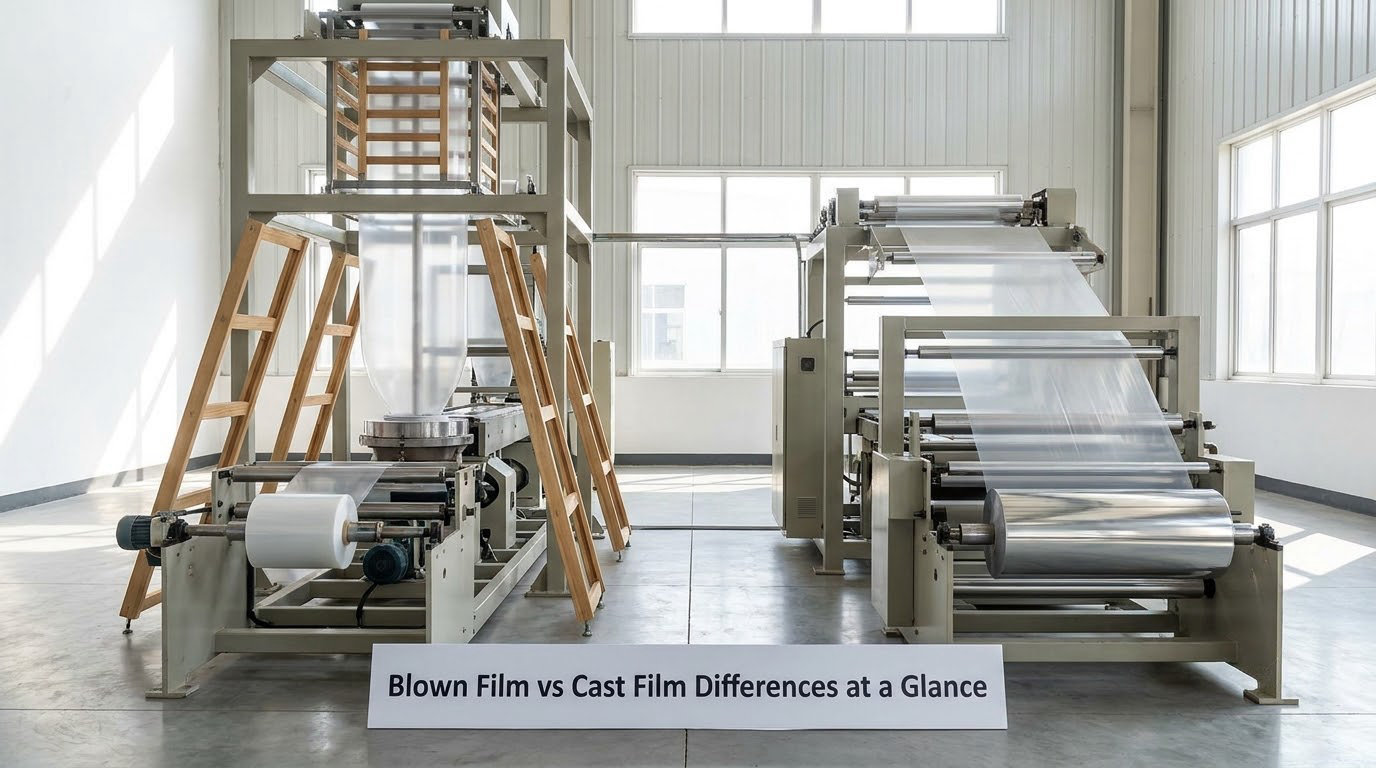
| Criterion | Blown Film | Cast Film |
|---|---|---|
| Resin handling | Same pellet feed, usually LLDPE, LDPE or blends | Same pellet feed, usually LLDPE, LDPE or blends |
| Forming process | Annular die, melt inflated with air into a film bubble | T-die or slot die, melt laid as a flat sheet |
| Cooling | Air ring and collapsing frame, gradual | Chill roll quench, near-instantaneous |
| Orientation | Biaxial, balanced in MD and TD | Largely machine-direction only |
| Typical gauge range | Roughly 1.5 to 4 mil for pallet wrap, up to heavier grades | Roughly 0.5 to 1.0 mil for hand and machine stretch film |
| Thickness control | Die gap plus air volume and haul-off speed | Die gap plus chill roll speed, very tight control |
| Mechanical properties | Higher tear and dart drop, better load memory | Lower tear, higher stretch capacity at break |
| Optical properties | More haze, lower gloss, thicker looking film | High clarity and gloss, thin looking film |
| Barrier performance | Lower WVTR and OTR at equal thickness because of the balanced structure | Better barrier per unit of mass but rarely produced below the thick gauges where it is needed |
| Surface and friction | Higher coefficient of friction, grips load, noisy on unwind | Lower coefficient of friction, slides easily, quiet on unwind |
| Heat sealing | Wider but softer seal window, higher seal initiation temperature | Narrower window, lower initiation temperature, cleaner seal on thin film |
| Output per line | Good at heavy gauges, limited by bubble stability at the top end | High at thin gauges, drops off fast as thickness rises |
| Relative cost | Higher cost per pound, often fewer pounds per wrapped pallet | Lower cost per pound, often more pounds per wrapped pallet |
| Typical applications | Heavy and irregular loads, construction products, bags and liners, agricultural mulch and silage wrap | Machine pallet wrapping, retail overwrap, food and pharma packaging, high-clarity film |
How Blown Film and Cast Film Are Manufactured
Blown film: the bubble process
Pellets go into the same kind of screw extruder in both processes, and the melt is homogenised and filtered before it reaches the die. Blown film then exits an annular die as a hollow tube, and compressed air through the bubble centre pushes the tube walls outward until the melt is stretched into a large cylinder called the film bubble.
Two ratios describe what just happened. The blow-up ratio is the bubble diameter divided by the die diameter, and it sets how much the film stretched around the tube. The draw-down ratio is the die gap divided by the final film thickness, and it sets how much the film was stretched vertically. Common practice is a draw-down ratio near one, which lets the air do the stretching.
Because the bubble is pulled in both directions at once, the film ends up stretched in the machine direction and the transverse direction together. That balanced structure is the reason blown film resists a tear from any starting direction, and it is the single technical fact behind most of the property differences on this page.
A collapsing frame folds the bubble flat, the flat tube passes through nip rolls, and the result is a lay-flat tube with a visible neck finish where the film was compressed. Winding then turns that tube into a roll. Any film produced with a bubble large enough to read as a bubble in the roll is blown film, which is why cut handles in grocery bags show that crease.
Cast film: the chill roll process
Cast extrusion sends the melt through a T-die as a flat sheet several times wider than it is thick. Instead of air, a large polished chill roll rotating at a controlled speed touches the melt and quenches it within fractions of a second. The rest of the roll is the cooling surface, and the film is trimmed at the edges before winding.
The quench rate is the story here. Film cooled that fast crystallises differently and comes out with high clarity, high gloss and a very low gauge capability, because the melt is being frozen into place rather than drawn down gradually.
The practical trade-off is orientation. A cast sheet is stretched as it is drawn off the chill roll in the machine direction, and essentially not at all across the width. That machine-direction-only structure gives long smooth elongation in one axis and weak, easy splitting tears in the other.
What the process means for equipment and control
A blown line needs a die with an adjustable lip gap, an air ring, a collapsing frame, nip rolls and a haul-off that can vary independently of the extruder. Stability depends on keeping bubble pressure, temperature and haul-off speed steady against each other, and a small disturbance shows up as a gauge band running the length of the roll.
A cast line needs a wider die, a very large chill roll, an oscillating haul-off or winder for roll quality, and often edge-trim reclaim. Control is more direct, but the melt has to stay above a fairly narrow temperature window or the roll surface and the optical quality suffer.
Thickness Control, Film Quality, and Consistency
Where gauge variation shows up downstream
On a blown line, gauge is set by die gap and by the balance between air volume, line speed and haul-off ratio. That gives a wide operating window and a wide tolerance, so cross-direction variation and gauge banding are the normal things to watch. A band that runs the full length of the roll means something upstream moved for a moment: resin temperature drift, a blower fluctuation, or a haul-off speed change.
On a cast line, the chill roll speed and haul-off ratio are the primary controls, and the rapid quench locks the surface quality in almost immediately. Cross-direction gauge is typically tighter and optically cleaner, so cast film is easier to print and easier to run through slitting and bag-making equipment at speed.
Surface defects also behave differently. Gels, specks and contamination pass through both processes, but in blown film they often show up as visible lumps in a highly stretched area of the bubble. Die lip build-up is more of a concern in cast extrusion because the lip runs close to the chill roll, and a deposit there prints across the full width of the sheet.
Rolled quality matters downstream as much as at the line. A telescoping or loosely wound cast roll causes problems in slitting and in unwind on a wrapper, while a badly formed neck finish on a blown roll makes bag-making equipment run poorly. Winding tension, tension taper and roll hardness are set on the winder, not by the die, on both routes.
The practical consequence for converters is that blown gauge variation is what determines how much waste a bag maker or shrink user has to allow for. Measure your own cross-web profile rather than trusting the nominal gauge, because the spread across the bubble is often wider than the spread across a cast sheet.
Strength, Stretchability, and Barrier Performance
Why blown film vs cast film tear strength differs
This is the biaxial orientation point again, and it explains most of the strength numbers you will see on a data sheet. In blown film, polymer chains are stretched around the bubble in both the machine direction and the transverse direction, so the structure is roughly balanced. A tear that starts in one direction meets a cross-oriented structure and has to work against fibres running across it.
Cast film is drawn off the chill roll almost entirely in the machine direction. Chains run long and aligned down the web, which is excellent for stretching a long way before failure, and poor at resisting a tear that runs with the web. The blown film vs cast film differences that turn up most often in incoming testing come straight from that structure: cast gives you more stretch capacity, blown gives you more tear and puncture resistance.
Dart drop impact tests reflect the same structure. Blown film carries more energy before puncturing, which matters when a load has a sharp edge, a protruding board corner or a strap buckle. Cast film, at the gauges it is normally run, deforms around a puncture and continues to wrap rather than stopping.
Load memory and load holding power are not the same measurement
Load memory is how well the film keeps trying to return to its original shape after you let go of the stretch. Blown film scores high here because of its balanced structure, and that is why it stays tight over a load for weeks in storage. Load holding power is a timed test at a fixed elongation and stretch ratio, and results vary with resin choice, gauge and film width.
Stretch capacity at break commonly lands somewhere between 150 and 200 percent for blown stretch film and 250 to 300 percent for cast, on comparable LLDPE. Those ranges are a useful sanity check when a supplier quotes you stretch film: a number far outside them usually means a very different resin or a different process.
Barrier performance depends on structure and gauge together
Oxygen and moisture transmission improve with a more crystalline, more balanced structure, which points in the same direction as blown film. At equal thickness blown film generally holds up better on gas and moisture transmission. The complication is gauge availability: barrier applications usually need film in the 40 to 60 micron range or above, which is a natural fit for a blown line and an awkward ask for a cast line.
For thin, print-then-seal structures where barrier matters less, cast film at 15 to 25 microns is the practical answer, and both routes are used this way in multi-layer coextrusion where the barrier layer is one of several. A modern stretch film structure can stack 30-plus layers, where older constructions used a handful, and the layer count does more for barrier than the process choice on its own.
Optical Properties, Sealability, and Processing Behavior
The most visible blown film vs cast film differences are optical. Cast film quenches so fast that the resulting structure scatters very little light, so you get low haze and high gloss and a film that looks almost like glass on a 20 micron gauge. Blown film is stretched through a thicker melt path and cools in free air, so it carries more haze and a lower gloss. It is not a defect, but on a retail or display pack it reads as a slightly dull, heavier film.
Friction behaves the same way. Blown film has a higher coefficient of friction, which means it grips a load and resists sliding, but it also means more force to pull off a roll, more noise in the warehouse, and sometimes a surface that fights against print rollers and labelling heads. Cast film slides past neighbouring layers with less resistance, which is why high-speed wrappers run it and why it is quieter in a trailer.
Heat sealing separates them as well. Blown film needs a higher sealing temperature and gives a wider window once it does seal, so it tolerates a lot of variation in the sealer. Cast film on a thin gauge seals at a lower temperature with less dwell, which suits form-fill-seal and small high-speed sealers, but the window is tighter and an overshot seal can distort the pack.
Printability leans to cast film. The surface is smoother, gauge is more even across the web, and corona treatment takes well, so flexo and gravure hold fine detail. Blown film prints, but the higher haze softens contrast and the wider cross-web gauge spread needs more make-ready on the plate or cylinder.
Shrink behaviour is worth separating too, because shrink film is a category rather than a process. You can blow a shrinkable formulation into a tube and you can cast one onto a chill roll, and what makes it shrink is the resin and the orientation, not the route through the die.
Production Speed, Changeovers, and Cost Comparison
Line output favours cast film at the thin end. A cast line runs high metres per minute at gauges from roughly 12 to 25 microns and stays stable, which is exactly what a high-speed pallet wrapper or an overwrap line needs. A blown line output falls away as you chase heavy gauges because the bubble has to be large and stable to make them, and bubble stability is the constraint you spend the most time managing.
At the thick end the picture reverses. Blown lines handle the 3 to 10 mil range that cast lines struggle to run at speed, so heavy duty bags, liners and agricultural film almost always come off a bubble. If your product is thick, the choice of process is usually made for you by the physics of the equipment.
Cost is where most published comparisons go wrong. Blown film generally costs more per pound, and quoting only that number makes it look like the expensive option. But if blown film is available at 80 or 100 gauge where the cast equivalent is 60 or 80, and both achieve the same load security, the higher gauge can win on pounds per pallet. The number to compare is cost per contained pallet, which includes film consumed, wrap cycles and rejected loads, not cost per roll or cost per pound.
Changeovers tell a similar story. Short runs and frequent gauge changes suit a cast line, where the die adjustment and speed change take seconds. A blown line holding a heavy bubble takes longer to stabilise and produces more start-up scrap. Conversely, a blown plant running one construction-grade product for months has very low scrap and very stable economics.
Market reality sits well inside that. Roughly 20 to 30 percent of stretch film is produced by blown extrusion and 70 to 80 percent by cast, because most stretch wrapping is thin and speed-driven, while the blown share concentrates in the heavy and specialty end. Labour and energy also separate slightly, since blowing a large bubble takes more air handling than laying a flat sheet.
Which Should You Choose?
| Choose blown film if | Choose cast film if |
|---|---|
| The load is heavy, irregular or has sharp edges and protrusions | The load is uniform, boxed and easy to wrap |
| Film needs load memory over weeks of storage | The pallet is wrapped and moved on the same day |
| You need gauge above roughly 1.5 mil | You need gauge below roughly 1 mil for output |
| Clarity is not the deciding factor | Clarity, gloss and print detail decide the spec |
| Unwind noise and slide resistance do not matter | High-speed wrappers and quiet warehouse environments matter |
| The film is bags, liners, agricultural, shrink or a barrier grade above 40 micron | The film is machine stretch wrap, retail overwrap, food, pharma or medical packaging |
| Long runs of one grade | Short runs, frequent gauge or grade changes |
A practical decision path starts with load shape. If a corner will touch the film, blown is the safer answer regardless of everything else. If the load is uniform and the wrapping machine runs fast, cast gives you more film per pound, less noise and a cleaner-looking pack.
Next is the gauge requirement, and this is where the two processes stop overlapping. Below about 1 mil, cast is the practical process. Above roughly 2 mil, blown is. In between, spec the load and the resin rather than the process.
Then look at the environment. Freezer and cold storage demand impact resistance and low creep, both of which point to blown film and to higher-density LLDPE blends. Ambient warehouse wrapping with a turntable or a robotic arm is the classic cast environment.
Finally, compare cost per contained pallet rather than per pound or per roll. The table above usually decides the matter, and it is the one calculation I would ask for before signing off on either film. For gauge specification, remember that 1 mil equals 25.4 microns, so 80 gauge is about 20 microns and 100 gauge is about 25 microns.
Frequently Asked Questions
Is blown film stronger than cast film?
Stronger depends on which property you mean. Blown film has higher tear, puncture and dart drop resistance because the bubble stretches the melt in two directions at once, which balances the structure in the machine and transverse directions. Cast film stretches further before it breaks, usually 250 to 300 percent against 150 to 200 percent for blown, because its chains align almost entirely in the machine direction.
Which process produces better optical clarity?
Cast film, without much argument. The chill roll quenches the melt almost instantly, which keeps crystallisation low and light scattering down, so cast film shows low haze and high gloss even at a gauge of 15 to 25 microns. Blown film cools gradually in free air after being stretched in the bubble, which leaves it hazier and slightly duller, though the haze is not a defect.
What film thickness is typically made with blown or cast extrusion?
Cast extrusion runs the thin end of the range, typically from about 0.5 to 1.0 mil, or 12 to 25 microns, where it holds high line speed. Blown extrusion covers the heavy end, typically from about 1.5 to 4 mil for pallet wrap and up to 10 mil for bags, liners and agricultural film. Somewhere around 1 to 2 mil the two processes overlap.
Can blown film and cast film use the same plastic resin?
Yes, in most cases. Both processes commonly run LLDPE, LDPE, metallocene grades or blends of them, and the resin choice is frequently closer to the final specification than the process. Process still decides what you get from that resin, since the bubble stretches it biaxially while the chill roll freezes it before transverse stretching can happen.
Which process is better for printing and heat sealing?
Cast film is generally the better choice for both. Its smoother surface, even gauge and higher gloss hold flexo and gravure detail, and a thin cast gauge seals at a lower temperature with less dwell on a form-fill-seal machine. Blown film seals across a wider temperature window once it reaches its higher initiation temperature, which gives it tolerance for less precise sealers.
How do manufacturers test the differences in film performance?
Converters typically test gauge across the web with a thickness gauge or a cut-and-weigh method, tensile and elongation on a tensile tester, tear and dart drop on impact equipment, coefficient of friction on a slip tester, and haze and gloss on a spectrophotometer. Barrier film is checked with oxygen and moisture transmission cells. Testing on your own loads beats a datasheet, because load shape changes the result.
Short version: choose blown film when the load fights back, and choose cast film when speed, clarity and thin gauge decide the economics. The blown film vs cast film differences that matter most in practice are tear resistance, load memory and available gauge, not resin or equipment brand.
Start by measuring one wrapped pallet of each candidate on your own line and comparing cost per contained load. That single test usually settles the argument faster than a spec sheet.